Hey everyone, let’s cut to the chase – if you’re running a hot dip galvanizing operation, you know that a wobbly kettle, wonky sinker arm, or unevenly leveled equipment isn’t just a minor annoyance. It’s the stuff that messes up zinc coverage, causes premature wear on parts, and can even throw your whole production schedule off. As a hot dip galvanizing equipment supplier, I’ve seen first-hand how skipping proper leveling turns a solid setup into a money pit way faster than a zinc spill. Today I’m walking you through exactly how to level your gear right – no fluff, no jargon, just what actually works. Metal Parts Hot Dip Galvanizing Equipment
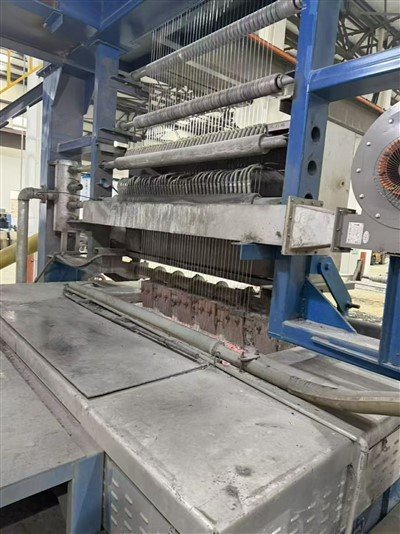
First, let’s get one thing straight: leveling hot dip galvanizing equipment isn’t just about using a level tool and calling it a day. This isn’t hanging a shelf in your garage. You’ve got a 50-foot-long kettle sitting in a pit full of molten zinc that’s at like 840°F – if it’s not level, the zinc will pool in low spots, leaving parts there with thick, crumbly zinc that’s hard to grind down, while high spots get barely any coating at all. I once had a customer call me panicking because their galvanized parts were failing a salt spray test in 200 hours, and turns out their kettle was 1.2 degrees off level. That’s all it took. So don’t skip the prep work, that’s where most people mess up.
Let’s start with the basics: what equipment are we leveling here? Most setups have three main bits: the kettle (obvi, where all the zinc melts), the work lift (the arm that hoists parts in and out, usually with a basket or hooks), and the flux tank pre-treat line. Each of these has different leveling needs, so you can’t just do one and call it done. I know some techs slap a level on the kettle and move on, but if your lift arm is tilted, it’ll drag parts on the tank walls, bend hooks, and even spill flux into the zinc – which is a whole other can of worms.
First step: prep the site. You can’t level a floppy concrete slab. If you’re installing new equipment, or re-leveling old stuff that’s shifted, the foundation is everything. For kettles, the pit needs to be dug extra deep, and the base should have at least 6 inches of reinforced concrete, no soft spots, no cracks. For older setups, check the slab for settling – I’ve seen pits where one side of the concrete dropped ¾ of an inch over 5 years because of poor drainage. Fix that drainage first, too – water in the pit will cause rust under the slab, which makes it shift. Clear the whole area around the equipment, no debris, no leftover zinc chunks that might throw off your level readings. Grab your tools: a good spirit level (not that cheap plastic one from the dollar store – get a 4-foot long aluminum level, or a laser level if you’ve got the budget, it’s worth it), a tape measure, a wrench (for adjusting jacks or leveling feet), and a notepad to write down readings – don’t trust your memory.
Now, let’s start with the kettle – that’s the big one. Wait until the kettle is cold, by the way. Leveling a hot kettle is a recipe for burns and wrong readings because metal expands when it’s hot, duh. Turn all the power off, drain any leftover zinc (if you can, even better – no molten metal sloshing around while you work), and let it sit for 24 hours minimum. Place your level on the top edge of the kettle – pick two opposite sides, front to back and left to right. Now, most kettles have adjustable leveling feet or screw jacks under each corner, right? Not all of them, but almost every modern unit we sell does, because we hate seeing customers struggle with this. Slowly adjust each jack, checking the level every few turns. Here’s the trick: don’t just get the “bubble in the middle” reading. For kettles, you want the level to be within 0.05 degrees across the entire length. Wait, what’s that in inches? About 1/16 of an inch per 10 feet. Yeah, that’s super precise, but that’s why the bad leveling happens. Most people stop at “bubble looks straight” and it’s off by a degree or two. If you’re using a laser level, you can set it to a reference line across the kettle top, so you can see exactly how much each side is off – way easier than reading a bubble.
Once the kettle’s level, move to the work lift. This is a mistake I see all the time: level the kettle, then forget the lift. The lift’s arm moves the parts in and out, and if it’s not level, when you lower a basket of parts into the zinc, one side dips further than the other. That means one side of the parts gets way more zinc, the other side is too high, so it barely coats. How to level the lift? First, make sure the lift is mounted to a solid column or frame – no wobble there. Extend the arm all the way out, and place your level on the main horizontal beam of the arm. If it’s off, adjust the mounting bolts or the lift’s base feet, same as the kettle. Also, test it: lower an empty basket into the flux tank, then the rinse tank, then the kettle. When you pull it out, check that the zinc level on the side of the basket is even all around. If one side has a thick line of zinc and the other is thin, your lift’s not level. That test takes 5 minutes and saves you hours of reworking bad parts.
Wait, what about smaller parts, like batch galvanizing lines vs. continuous lines? Continuous lines are a bit different. For continuous lines, you’ve got the kettle, the lift, and the entry/exit conveyors. The conveyors need to be level too, because if they tilt, parts will stick, jam, or not feed straight into the kettle. Same rule applies: level left-right and front-back, check with the level tool, adjust feet as needed.
Now, the part most people skip after leveling: securing and testing. Once you think everything’s level, tighten all the bolts on the jacks, the lift mounts, the conveyor frames – don’t skip this, because when you fire up the kettle and it gets hot, the metal expands, and if the bolts are loose, the whole thing will shift. Then, do a test run: run a full batch of test parts, simple ones like washers or small brackets, nothing too complex. Inspect each part: check the zinc coverage, no thin spots, no thick drips, no bare metal. Measure the zinc thickness with a gauge if you have one – that’s the real way to tell if leveling worked, not just a visual check. If the test parts are good, you’re golden. If not, go back and recheck the level – something shifted when you tightened the bolts, or you missed a spot.
Oh, and one more thing for ongoing maintenance: don’t wait years to re-level. Zinc kettles wear over time, the foundation can settle, jacks can loosen. I recommend re-leveling every 6 months for high-production lines, once a year for smaller operations. Also, after any major repair – like patching a hole in the kettle or replacing a lift arm – always re-level. I had a customer last year who replaced a bent lift arm, then didn’t re-level, and their first batch came out with half the parts having no zinc on the bottom edge. They were this close to blaming the zinc supplier, until we walked through it and caught the bad leveling.
Here’s the hard truth: if your equipment is not level, you’re wasting zinc, you’re wasting time reworking parts, and you’re risking downtime from failed batches. I know it’s tempting to just jump into production instead of spending a few hours leveling, but that 2 hours now will save you days of headaches later.
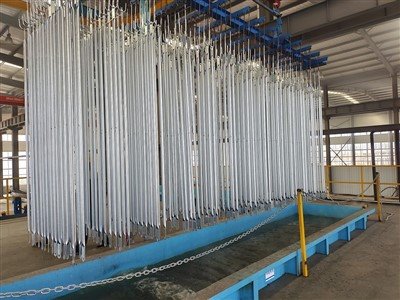
If you’re setting up a new galvanizing line, or you’re dealing with a setup that’s been giving you grief, hit us up for a chat. We don’t just sell equipment – we’ve spent years helping small and large ops get their leveling right, so their galvanizing is consistent, their parts pass tests, and their profits stay where they belong. Don’t guess at your leveling – get it right the first time, so you can focus on growing your business, not fixing avoidable mistakes.
Hot Dip Galvanizing Equipment REFERENCES
- Hot Dip Galvanizing Equipment Installation and Operation Manual. Industrial Zinc Association, 2021.
- Leveling and Alignment Guidelines for Industrial Metal Processing Equipment. National Association of Metal Finishers, 2020.
- Best Practices for Maintaining Hot Dip Galvanizing Process Consistency. Galvanizers Association of Canada, 2022.
Jinzhou Hongri Galvanizing Equipment Co., Ltd.
As one of the most professional metal parts hot dip galvanizing equipment manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy durable metal parts hot dip galvanizing equipment for sale here from our factory. We also accept customized orders.
Address: Yingpan Industrial Park, Taihe District, Jinzhou City. Address: No. 90, Gongwei Street.
E-mail: rsea.jz@163.com
WebSite: https://www.hrgalvanize.com/
