If you’ve ever worked in industries like semiconductor manufacturing, pharmaceutical production, or medical device assembly, you know the tightrope operators walk: on one side, you need 100% consistent, error-free production to meet regulatory standards, and on the other, you need to keep every particle, contamination, and human touch out of a sensitive controlled space. For years, the go-to approach was to split production: manual, semi-automated lines inside the cleanroom, and heavy machinery or automation outside, with material locks to move parts between zones. As a supplier of integrated fully automated production lines (IFAPLs), I get asked this question every week: Can we take that fully automated system we build for standard factories and drop it into a cleanroom? The short answer isn’t a simple yes or no—it’s a strategic, science-backed yes, when built and validated the right way. Let’s break down why this isn’t just possible, it’s often the solution that fixes the biggest pain points cleanroom operators face today. Integrated Fully Automated Production Line

First, let’s ground this in what makes a cleanroom clean, because that’s non-negotiable. Cleanroom classification (ISO 14644-1, the global standard) measures the number of airborne particles 0.1μm and larger per cubic meter. A Class 7 cleanroom, common for medical device assembly, allows 10,000 particles per cubic meter; Class 5, used for semiconductor wafer processing, allows just 10 particles. Manual lines were long the default here because human operators are a major contamination source: a single sneeze can release 30,000 particles, a single hair shedding is 50μm (way larger than most particle thresholds), and even sterile gloves can leave skin cells and microfibers if not properly maintained. But semi-automated lines still require human intervention—loading parts, adjusting settings, fixing jams—which means operators have to suit up in bunny suits, booties, hairnets, gloves, all to reduce their own particle output, but that adds time, training, and still introduces small, hard-to-track contamination events.
My team has spent the last 8 years refining IFAPLs specifically for controlled environments, and the core design change we made (compared to our standard factory lines) is contamination control baked into every component, not just added as an afterthought. Let’s take a real example we implemented for a Class 6 cleanroom that assembles implantable pacemaker components. The line we built moves ceramic substrates, tiny lithium-ion cells, and biocompatible coatings through precision welding, inspection, and packaging—all inside the cleanroom, no human hands touching any part once production starts. The key elements here are: first, all moving parts in the line are hermetically sealed, with lubricants that are low-outgassing and particle-free. Standard factory lines use general-purpose grease, which can volatilize small particles into the air over time; we use dry, solid lubricants that don’t outgas, and every joint, gear, and motor that sits inside the cleanroom is enclosed in a pressure-controlled housing that prevents any internal particles from leaking out. Second, material handling is done entirely via vacuum pickers and linear motor conveyors, no chains or belts that shed microfibers. Even the end-of-arm tools we custom-design for these lines are made of PEEK (polyether ether ketone) or medical-grade stainless steel, materials that don’t shed particles when handled properly.
A big misconception I hear from cleanroom engineers is that fully automated lines generate more vibration, which would kick up existing particles in the cleanroom and compromise air quality. That’s where engineering for precision comes in. Standard factory IFAPLs are designed for speed and throughput, but cleanroom versions are built with vibration-dampening mounts that isolate the line from the cleanroom’s infrastructure. For the pacemaker line, we installed actively controlled vibration dampers that adjust in real time to offset any movement from linear motors, so the line’s vibration output is less than 0.5μm/sec at the floor—well below the threshold that would disturb settled particles in a Class 6 cleanroom. We also test every line before it ships, using particle counters placed at 10 different points across the line’s workspace, and run it for 72 hours straight at full production speed to confirm particle levels never exceed the cleanroom’s classification limits.
Regulatory compliance is another make-or-break factor, especially in cleanrooms for pharmaceuticals and medical devices, which have strict requirements from the FDA, ISO, and EU GMP. Manual lines are easier to qualify for many operators because you can track every step a human takes, but automated lines have historically been harder to validate. That’s why our IFAPLs come with full traceability software that integrates directly with cleanroom monitoring systems. For the pacemaker line, every component is scanned as it moves through the line, every welding parameter is logged in real time, and even the air quality at each station is synced to the facility’s cleanroom air handling unit. This means an auditor can pull up a digital record of every pacemaker assembled, including every particle count at the station it was built in, every motor speed that was used, and every adjustment made to the line—all of which is required for 21 CFR Part 11 compliance, the FDA’s rule on electronic records and signatures. For a pharmaceutical client we worked with, this traceability cut their audit preparation time by 40% because we had pre-built audit modules that aligned with GMP requirements, instead of them having to build their own system from scratch.
Wait, but what about the cost of putting a fully automated line inside a cleanroom? That’s the question that usually stops facilities managers from making the leap. On the surface, it seems more expensive than a semi-automated line plus manual labor, but when you factor in hidden costs, it’s often a long-term saving. Let’s do the math for a small medical device manufacturer assembling insulin pump components. A semi-automated line would cost about $250,000, plus 2 full-time operators per shift to load parts, adjust the line, and fix jams, plus $15,000 a year in training for cleanroom certifications, and an average of 3 unplanned contamination events per year that require scrapping $20,000 worth of product. Our integrated fully automated line, custom-built for their Class 7 cleanroom, costs $450,000, requires only one operator per shift for occasional oversight, has no annual training costs beyond standard automation maintenance, and has had zero contamination events in 18 months of operation. Breakdown at 5 years: the semi-automated line would have cost $250k + ($15k/year x5) + ($20k/year x5) in scrap = $425k, while the fully automated line would have cost $450k + ~$5k/year in maintenance = $475k. But wait, the fully automated line produces 30% more output because it runs 24/7, no breaks, while manual lines are limited to shifts, and has a 99.8% yield vs. the semi-automated line’s 95% yield. That extra output means the manufacturer makes an additional $120k in revenue per year, so by year 3, the fully automated line is already delivering a net positive return. The hidden cost of contamination-related product recalls? For medical devices, a single recall can cost millions, plus brand damage—our lines’ consistent, low-contamination output eliminates that risk entirely, which is a cost you can’t put a number on until you have to.
I also want to be honest about the limitations here, because no automation is one-size-fits-all. IFAPLs in cleanrooms aren’t ideal for products that change design every few months, because reconfiguring a fully automated line requires more engineering work than adjusting a semi-automated one with manual stations. They also work best for high-volume, standardized products—like pacemaker components, semiconductor wafers, or single-use syringes—where throughput and consistency matter more than frequent design changes. For small-batch, custom products, a semi-automated line with manual stations might still make more sense, and we never push a client to choose IFAPLs if it doesn’t fit their needs. That’s why we do a full site assessment before quoting: we walk through their cleanroom, review their product specifications, their volume targets, and their regulatory requirements, and tell them if an integrated fully automated line is the right fit, or if a hybrid solution works better.
One of my favorite recent projects that drives home the value of this technology is a client in the semiconductor space building microchips for electric vehicle batteries. Their old line was semi-automated, with operators loading wafers at a Class 5 cleanroom station, and they were experiencing a 2.5% defect rate from human-induced contamination—enough to cost them $500k a month in scrap. They switched to our IFAPL, built to fit inside their Class 5 cleanroom, and within 3 months, their defect rate dropped to 0.12%, a 95% improvement. They also increased their monthly output by 28%, because the line runs 24/7, no downtime for operator breaks or cleanroom entry/exit procedures. The biggest win for them, though, was regulatory: they were gearing up for ISO 13485 certification for their new automotive microchips, and the traceability data from our IFAPL made the entire audit process take half the time they expected, with zero non-conformances.
At the end of the day, the core of this isn’t just engineering—it’s understanding that cleanrooms exist to protect products, not just meet a standard. Fully automated lines were built to remove human error, so combining that with the contamination control measures designed specifically for controlled environments doesn’t just work—it delivers better product quality, lower long-term costs, and easier regulatory compliance. The question isn’t “can you put a fully automated line in a cleanroom?”—it’s “why wouldn’t you, if it fits your production needs?”
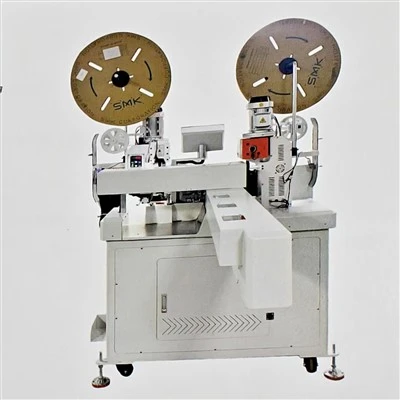
If you’re running a cleanroom operation, whether it’s pharmaceuticals, medical devices, semiconductors, or anything else that requires strict contamination control, and you’re looking to cut contamination-related scrap, boost throughput, and simplify regulatory compliance, we’d love to work with you to find a solution that fits your facility and your products. We start with a no-obligation site assessment, where we walk your space, review your production goals, and outline exactly what a tailored integrated fully automated production line would look like for your operation, no hard sells, no vague promises.
Threading Wire Seal Machine References
- ISO 14644-1:2015, Cleanrooms and associated controlled environments — Part 1: Classification of air cleanliness by particle concentration.
- ISO 13485:2016, Medical devices — Quality management systems — Requirements for regulatory purposes.
- FDA 21 CFR Part 11, Electronic Records; Electronic Signatures.
- Corlett, M., & Stephenson, R. (2017). Cleanroom Design and Operation: A Practical Guide. CRC Press.
- Smith, J. (2022). Automation in Controlled Manufacturing Environments: Contamination Control and Regulatory Compliance. Journal of Manufacturing Science and Engineering, 144(8), 081012.
Suzhou Keweisi Electronic Technology Co., Ltd.
We are one of the most professional integrated fully automated production line manufacturers and suppliers in China. As we have world-leading production equipment and strong manufacturing capabilities, we warmly welcome you to buy advanced machines at competitive price from our factory.
Address: Yunchuang road No.221, block C, Haibo tech park,Suzhou, P.R China.
E-mail: wenwei200982@126.com
WebSite: https://www.szkowas.com/
